
Rotary Die‑Cutting in In‑Mould Label Production: A Detailed Overview
Rotary Die‑Cutting in In‑Mould Label Production: A Detailed Overview
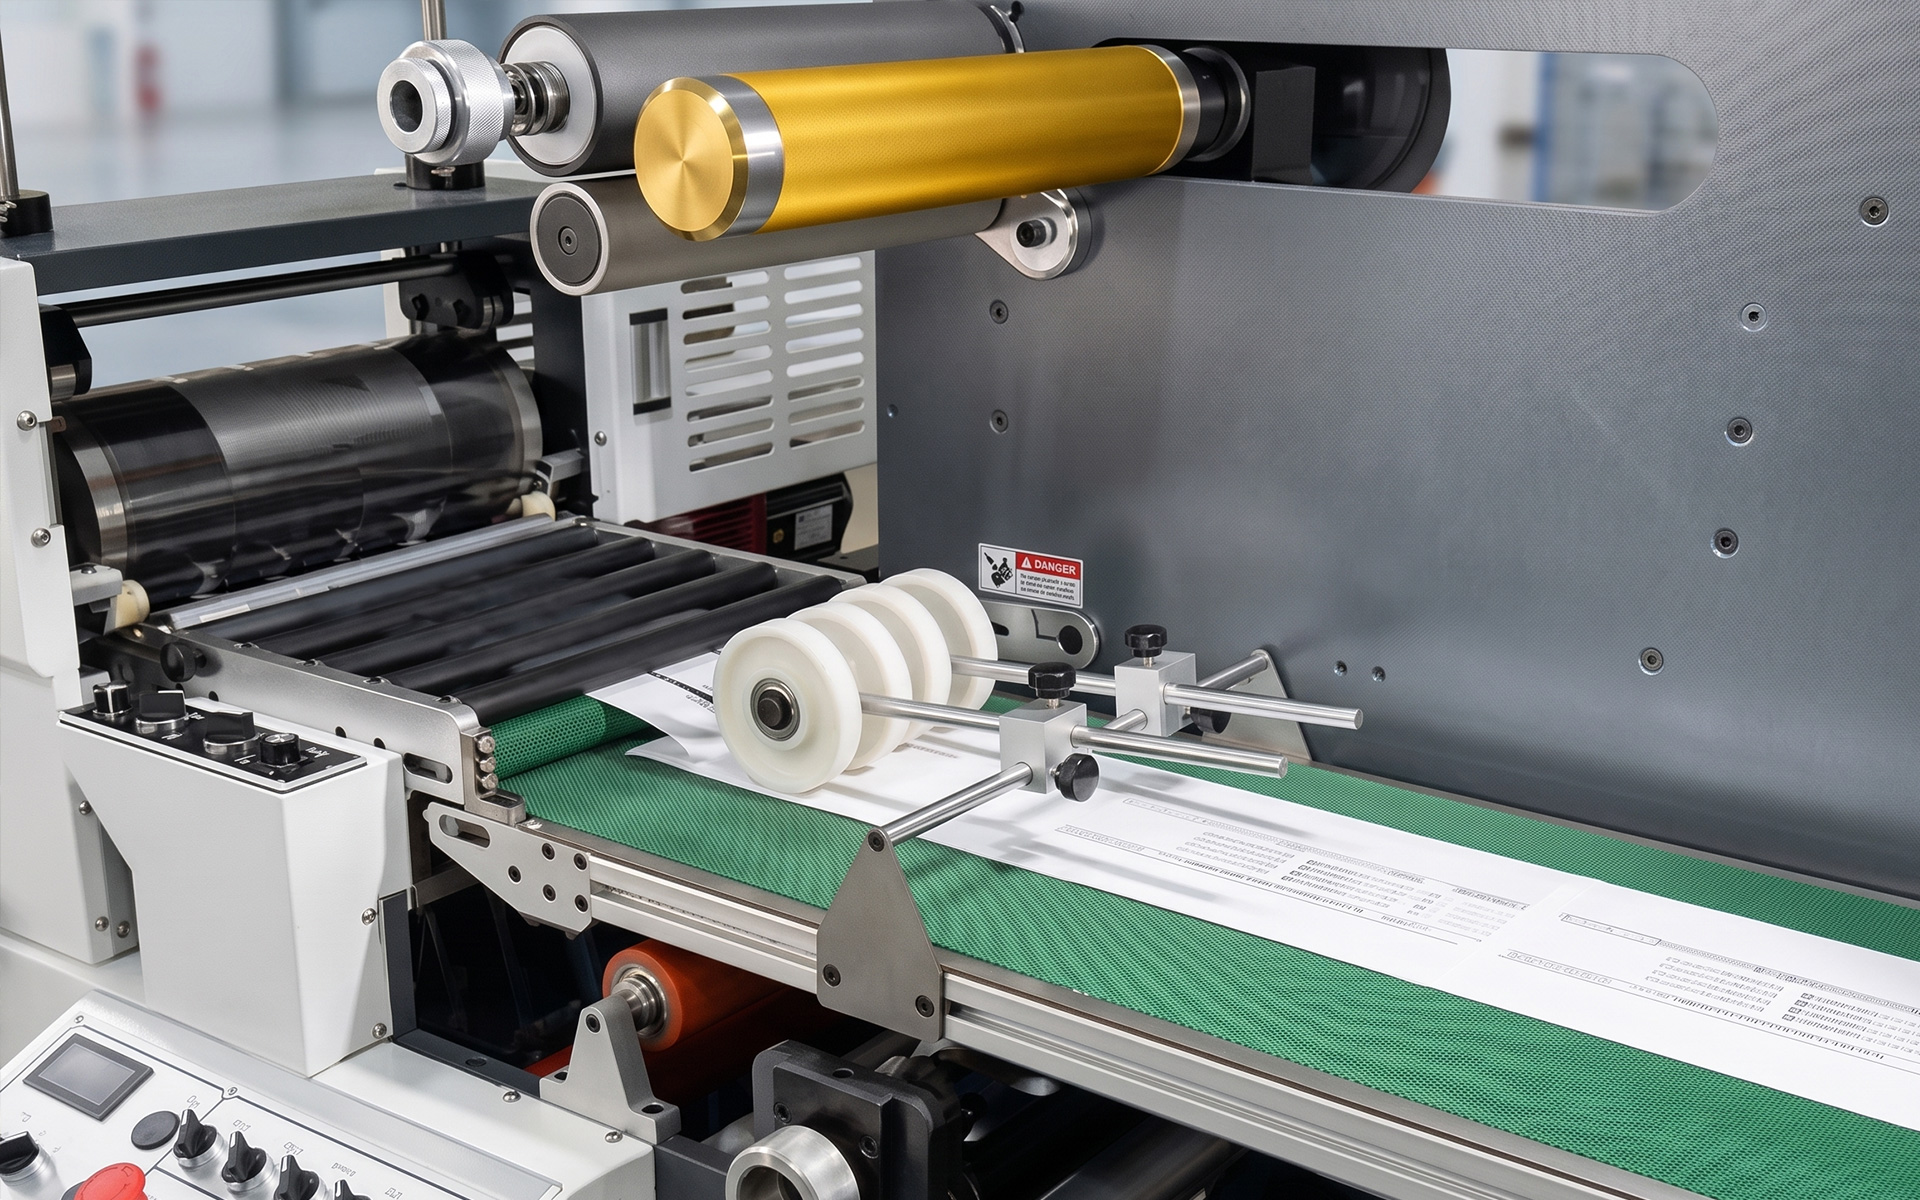
In the die‑cutting stage of in‑mould label (IML) manufacturing, rotary die‑cutting is the mainstream technology for high‑volume production. Unlike traditional flatbed die‑cutting, rotary die‑cutting uses a cylindrical die and cuts the material continuously as it passes between the die cylinder and an anvil roll. This “rolling shear” principle brings outstanding advantages: extremely high speed, high accuracy, and functional integration, making it the preferred choice for large‑batch, high‑precision IML label orders. This article comprehensively analyses rotary die‑cutting technology, covering its working principle, equipment components, key advantages, limitations, and typical applications.
1. Working Principle: Continuous Rotating “Rolling Shear”
The core of rotary die‑cutting consists of a cylindrical die (die cylinder) and an anvil roll. The die cylinder has cutting rules (or integral blades) that match the label contour; the anvil roll has a smooth, hard surface (or a soft blanket). During operation:
Continuous web feed: The roll‑fed IML material passes at constant speed between the two rolls.
Rotary cutting: The die cylinder and anvil roll rotate synchronously. When the cutting rule contacts the anvil roll, it cuts completely through the material.
Continuous output: The cut labels and waste skeleton separate automatically. Finished labels are collected by a conveyor or vacuum system, while the waste skeleton is rewound.
The entire process is continuous, without stops, and the cutting speed is limited only by web speed and rotational capability. This principle is similar to rotary printing, which is why it is also called “rotary die‑cutting”.
2. Main Equipment Components
A complete rotary die‑cutting unit typically includes:
| Component | Function |
|---|---|
| Die cylinder | Cylindrical die with integral cutting rules. Materials: tool steel (case‑hardened), carbide, or magnetic base roll with flexible dies. |
| Anvil roll | Provides backup for cutting. Chrome‑plated or coated; for certain materials, a plastic blanket can be used. |
| Servo drive system | Synchronises die cylinder with printing units or pull rolls for accurate registration. |
| Waste rewind shaft | Automatically rewinds the waste skeleton after cutting. |
| Finished label collection system | Conveyor belt, vacuum, or air blast to collect finished labels. |
| Static eliminator | Removes static charge generated during cutting to prevent label sticking. |
In inline production, the rotary die‑cutting unit is usually installed at the end of a flexographic or gravure printing line, creating an integrated process: printing → varnishing → die‑cutting → waste stripping → rewinding.
3. Key Advantages
3.1 Very high speed – ideal for large batches
Because of continuous operation, rotary die‑cutting is much faster than flatbed. Typical speeds match printing speeds: 200–400 m/min (in terms of label output, far exceeding flatbed’s tens per minute). For annual volumes exceeding one million labels (e.g., laundry detergent bottle labels, lubricant pail labels), rotary die‑cutting is the only way to keep up with production demands.
3.2 High cutting accuracy
The line contact between die cylinder and anvil roll provides more uniform pressure than the area contact of flatbed. Combined with high‑precision servo drives and closed‑loop registration control, rotary die‑cutting achieves ±0.1 mm or better repeatability. This is critical for transparent labels, fine borders, or small text that must align precisely with printed graphics.
3.3 Functional integration – multiple processes in one pass
Multiple rotary die‑cutting stations can be arranged in series to perform in one pass:
Die‑cutting (main contour)
Perforating (e.g., hang holes)
Creasing (for folding or label positioning)
Embossing (surface texture)
Kiss cutting (for liner‑based labels – but IML requires full cut)
This integration greatly reduces inter‑stage handling and registration errors.
3.4 Fully automatic waste stripping – labour saving
In rotary die‑cutting, the waste skeleton separates naturally during continuous motion: the waste is rewound continuously, while finished labels are conveyed away. No manual intervention is needed, making it ideal for high‑speed, automated production.
3.5 Long tool life
Rotary die cylinders can be made of carbide or use magnetic sheet‑type dies with hardened steel blades (hardness HRC 60–65). Under normal use, a rotary die can last for millions of cuts – far longer than flatbed steel‑rule dies. For long‑running jobs, the tooling cost per label is much lower than repeatedly replacing flatbed dies.
4. Limitations and Challenges
4.1 High tooling cost
Manufacturing a rotary die cylinder requires precision machining (CNC engraving, EDM), heat treatment, and surface coating. A single die cylinder can cost from several thousand to tens of thousands of CNY. For magnetic die systems, the initial base roll is still expensive, though replacement flexible dies are cheaper. Therefore, rotary die‑cutting is not economical for small batches (e.g., less than 100,000 labels) and is best suited for long‑run, high‑volume orders.
4.2 Long changeover time – lower flexibility
Changing a rotary die typically takes 30–60 minutes, including removing the old cylinder, cleaning, installing the new one, and adjusting pressure and registration. In contrast, flatbed die change takes only 5–10 minutes. Thus, rotary die‑cutting is not suitable for environments with frequent job changes.
4.3 High demands on material uniformity
Rotary die‑cutting is a continuous rolling shear process. It requires consistent material thickness, stable tensile properties, and good tension control. If the film thickness varies greatly (e.g., recycled composite films), local areas may not cut through or may cut through too deeply. Also, web stretching can affect registration, requiring automatic tension control and edge guiding.
4.4 High initial equipment investment
A rotary die‑cutting unit (especially an inline configuration) costs significantly more than a flatbed cutter. Beyond the die cylinder itself, it requires precision servo drives, registration systems, waste rewind, and more. For small converters or companies new to IML, the entry barrier is high.
5. Typical Applications in IML
Rotary die‑cutting is used for large‑batch, high‑precision, high‑efficiency IML label production. Common examples:
| Application Area | Typical Products | Annual Volume (reference) |
|---|---|---|
| Household / laundry | Laundry detergent bottles, dishwashing liquid bottles | Millions to tens of millions |
| Lubricants | 4L/1L engine oil pails | Millions |
| Food & beverage | Yogurt cups, ice cream tubs, beverage bottles | Millions |
| Personal care | Shampoo bottles, body wash bottles | Millions |
| Pharma / nutraceuticals | Pill bottles, supplement jars | Hundreds of thousands to millions |
6. Comparison: Rotary vs. Flatbed Die‑Cutting
| Aspect | Rotary Die‑Cutting | Flatbed Die‑Cutting |
|---|---|---|
| Speed | 200–400 m/min (continuous) | 20–80 strokes/min (intermittent) |
| Tooling cost | High (thousands–tens of thousands CNY) | Low (tens–hundreds CNY) |
| Die change time | 30–60 minutes | 5–10 minutes |
| Cutting accuracy | ±0.1 mm or better | ±0.2–0.5 mm |
| Material uniformity requirement | High | Moderate (adjustable via make‑ready) |
| Waste stripping | Fully automatic | Requires auxiliary or manual |
| Functional integration | Strong (multiple stations in series) | Weak (single cut only) |
| Suitable batch size | >100,000 pieces | Thousands to tens of thousands |
| Tool life | Millions of cuts | Tens to hundreds of thousands |
7. Inline vs. Offline Modes
Rotary die‑cutting can be configured as inline or offline:
Inline mode: The die‑cutting unit is installed at the end of the printing line. Printing, varnishing, die‑cutting, and waste stripping are completed in one pass. This is the most efficient method for large batches, eliminating intermediate rewinding and re‑registration errors.
Offline mode: Printing is done first and rewound; then the roll is transferred to a standalone rotary die‑cutter. This is used when printing and cutting speeds do not match, or when die‑cutting is done at a different location, but it adds handling steps.
High‑performance rotary die‑cutting systems from brands such as MOTEK, Bernal, RotoMetrics, etc., typically offer inline/offline switchability and integrate automatic registration and fine pressure adjustment to accommodate different materials.
8. Conclusion
Rotary die‑cutting, with its high speed, high precision, and high automation, has become the irreplaceable converting technology for large‑scale IML label production. Although tooling and equipment costs are higher, for stable, long‑running large batches, the gains in productivity, lower reject rates, and labour savings more than justify the initial investment. As IML labels continue to penetrate daily chemical, food, pharmaceutical, and other markets, and as technology advances (magnetic dies, quick‑change systems), rotary die‑cutting will become even more widespread.
For label converters, a rational strategy is: use rotary die‑cutting for long runs and high volumes; keep flatbed die‑cutting for short runs, prototypes, and emergency jobs. The two complement each other, enabling optimal capacity utilisation and cost control in the die‑cutting process.
Contact Us
Name*
Telephone*
Region*
Please fill in your request*


