
Solventless Lamination Process in the Production of In-Mould Labels
Solventless Lamination Process in the Production of In-Mould Labels
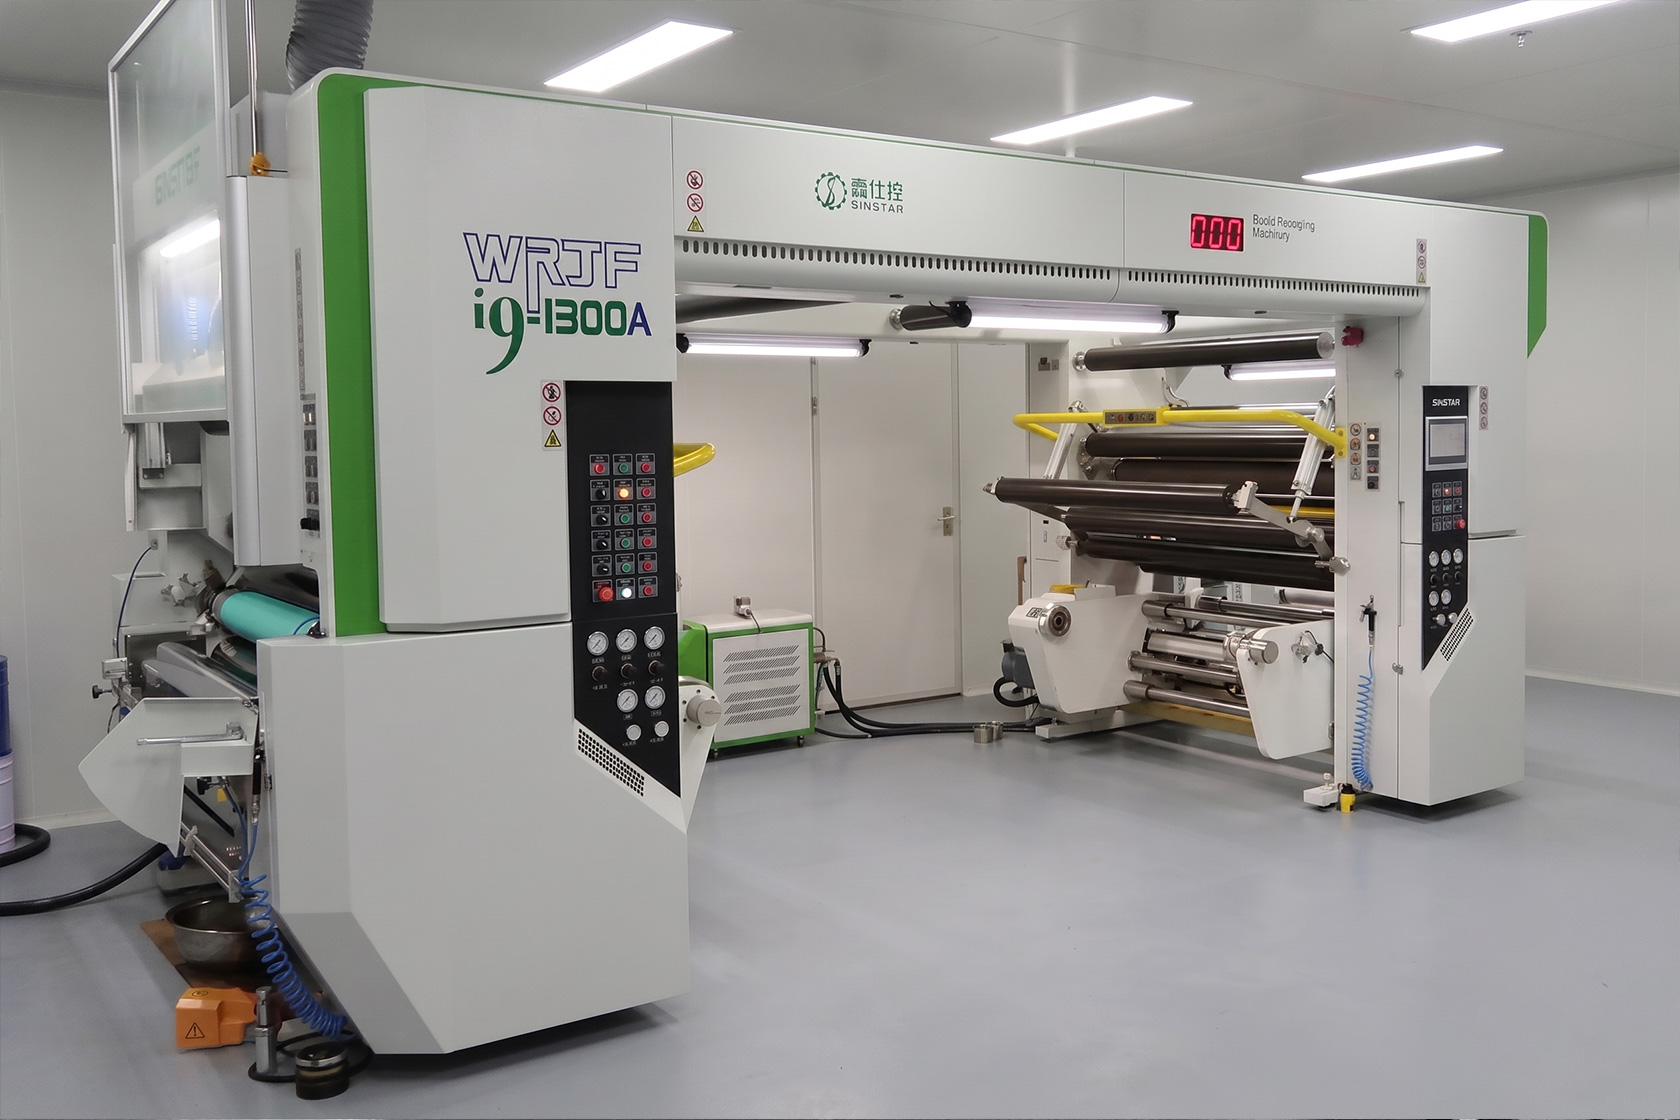
In the multi‑layer lamination technology system for in‑mould labels (IML), dry lamination was once the mainstream process for bonding heterogeneous materials, but the VOC emissions from its solvent‑based adhesives have become increasingly restricted by environmental regulations. As an environmentally friendly upgrade to dry lamination, solventless lamination (also known as solvent‑free lamination) has emerged. This process uses 100% solids adhesives, which are applied and immediately pressed together without the need for oven drying, achieving zero VOC emissions, low energy consumption, and high productivity. This article systematically introduces the solventless lamination process, covering its principles, key control parameters, typical applications in IML, advantages and disadvantages, and development trends.
1. Basic Principle and Process Flow of Solventless Lamination
1.1 Principle
The core of solventless lamination is the use of liquid adhesives containing no organic solvents. The most common type is two‑component polyurethane (PU) adhesive, consisting of a polyol component (Part A) and an isocyanate component (Part B). The two components are mixed online at a certain ratio (typically 100:50 to 100:75) before coating, then applied to the substrate surface. At room temperature or under mild heating, Parts A and B undergo a chemical reaction (crosslinking curing), forming a strong adhesive layer. Since no solvent evaporates, all solid components of the adhesive remain in the glue line; therefore, although the coating weight per unit area is lower than that of solvent‑based systems, the dry film thickness is sufficient.
1.2 Typical Process Flow
A solventless lamination line typically consists of the following units: first substrate unwind → solventless coating unit (mixing and coating) → laminating unit → wind (with optional in‑line or off‑line curing). The detailed steps are:
Mixing and coating: Parts A and B are delivered by precision metering pumps to a static mixer before the coating head, where they are mixed uniformly. The mixture is then applied evenly onto the first substrate using a five‑roll solventless coating head or a three‑roll coating head. Coating weight is typically controlled at 0.8–2.5 g/m² (only one‑third to one‑half that of solvent‑based systems).
Lamination: The coated first substrate immediately meets the second substrate at the laminating nip and is bonded under pressure. Because there is no drying section, the lamination process is extremely short (less than one second from coating to pressing).
Curing: The wound laminate is placed in a curing oven (30–50°C, controlled humidity) for 24–48 hours to allow full crosslinking of the adhesive, achieving final peel strength. Some new adhesives offer “instant strength,” eliminating the need for curing before subsequent processing.
1.3 Key Equipment Features
Solventless coating head: A closed five‑roll or three‑roll system that precisely controls coating weight and prevents the adhesive from absorbing moisture from the air.
Mixing system: Equipped with high‑precision metering pumps (gear pumps or piston pumps) with flow control accuracy of ±1%, ensuring a constant mix ratio.
Laminating unit: The heated nip roll temperature is adjustable (30–60°C) to accelerate the initial reaction and improve initial tack.
2. Process Characteristics and Key Parameters
2.1 Core Advantages
Zero VOC emissions: Completely free of organic solvents, no drying tunnel required, no exhaust gas treatment cost – meets the strictest environmental standards.
Low energy consumption: No need to heat large volumes of air to evaporate solvents; energy consumption is only 20–30% of solvent‑based dry lamination.
High productivity: Lamination speeds can reach 300–400 m/min (or even higher), far exceeding solvent‑based dry lamination (typically 150–250 m/min).
Adhesive saving: Coating weight is only 30–50% of solvent‑based systems (on a dry basis), significantly reducing adhesive usage.
Safe and hygienic: No solvent residue, no fire or explosion risk – suitable for food and pharmaceutical packaging.
2.2 Key Process Parameters
| Parameter | Typical Range | Impact |
|---|---|---|
| Mix ratio | 100:50–100:75 (A:B) | Deviation leads to incomplete curing or tacky adhesive layer |
| Coating weight | 0.8–2.5 g/m² | Too low: insufficient strength; too high: increased cost, possible strike‑through |
| Lamination speed | 150–400 m/min | Affects initial tack and pot life management |
| Lamination roll temperature | 30–60°C | Accelerates reaction, improves initial bond |
| Curing temperature | 30–50°C | Determines curing speed and final strength |
| Curing time | 24–48 hours | Adjustable based on adhesive type and temperature |
2.3 Pot Life and Operating Window
After mixing, the viscosity of solventless adhesive gradually increases over time until it can no longer be applied. This period is called the “pot life,” typically 20–60 minutes. Production must match coating speed with the amount of mixed adhesive to prevent gelling in the coating pan.
3. Application of Solventless Lamination in IML
In the IML field, solventless lamination is mainly used in the following scenarios:
3.1 High‑End Food IML Labels
For packaging that comes into direct contact with food or sensitive food products (e.g., yogurt cups, ice cream tub labels), any solvent residue poses a migration risk. Solventless lamination completely avoids solvent residues such as ethyl acetate and toluene, complying with food contact material regulations such as GB 9685 and EU 10/2011. For example, when producing IML labels with the structure “printed PET film / solventless adhesive / PE heat‑seal layer,” solventless lamination ensures the label is safe and reliable under hot‑fill or refrigerated conditions.
3.2 Pharmaceutical IML Labels
Pharmaceutical packaging is extremely sensitive to solvent residues. Solventless lamination meets the stringent hygiene requirements of medicinal packaging, preventing organic solvents from migrating into the drug. Typical applications include the lamination of PET facestock, aluminium foil barrier layer, and PE heat‑seal layer (e.g., IML labels on the bottom of blister packs).
3.3 Solvent‑Sensitive Film Materials
Certain high‑performance films (e.g., fluoropolymer films, PVDC‑coated films) may be swollen or corroded by organic solvents. Solventless lamination uses 100% reactive adhesives with no solvent attack, making it suitable for such special substrates.
3.4 PE/PE Homogeneous Lamination (Recyclable Design)
In the manufacture of all‑PE IML labels, two layers of PE film need to be laminated together. Solventless lamination uses polyurethane adhesive, which – unlike direct heat fusion co‑extrusion – still provides adequate peel strength. With a very low coating weight (approx. 1–2 g/m²), its impact on the quality of recycled material is minimal. This is one of the viable options for achieving “all‑PE mono‑material IML labels.”
4. Advantages and Disadvantages Analysis
4.1 Advantages
| Advantage | Description |
|---|---|
| Environmentally friendly | Zero VOC emissions, no exhaust treatment needed – complies with clean production requirements |
| Low energy consumption | No drying tunnel; electricity and heat consumption greatly reduced |
| High speed | 300–400 m/min, increasing productivity |
| No solvent residue | Safe and hygienic – suitable for food/pharmaceutical packaging |
| Adhesive saving | Coating weight only 1/2 to 1/3 of solvent‑based systems |
| Small equipment footprint | No long drying tunnel; line length reduced by about one‑third |
4.2 Disadvantages
| Disadvantage | Description |
|---|---|
| High initial equipment investment | Solventless coating head and precision mixing system are expensive |
| Slightly higher adhesive cost | Solventless PU adhesive unit price is generally higher than solvent‑based (but lower coating weight means total cost may be close or slightly lower) |
| High process control requirements | Mix ratio, temperature, and pot life must be precisely controlled |
| Sensitivity to substrate wettability | For very low surface energy materials (e.g., PTFE, untreated PE), corona treatment or primer may be required |
| Low initial tack | Immediately after lamination, bond strength is low; careful handling is needed to avoid shifting |
5. Comparison of Solventless Lamination, Dry Lamination, and Extrusion Lamination
| Process | Adhesive/Medium | Environmental Friendliness | Speed | Coating Weight (dry) | Equipment Investment | Bond Strength | Main Applications |
|---|---|---|---|---|---|---|---|
| Solventless lamination | 100% solids 2K PU | Excellent (zero VOC) | 300–400 m/min | 0.8–2.5 g/m² | Medium‑high | High | Food/pharmaceutical IML, heterogeneous materials |
| Solvent‑based dry lamination | Solvent‑based PU (ethyl acetate, etc.) | Poor (VOCs) | 150–250 m/min | 2–5 g/m² | Medium | Very high | General purpose, but under environmental pressure |
| Extrusion lamination | Molten resin (LDPE/EVA) | Excellent (solvent‑free) | 50–250 m/min | 10–50 μm (approx. 10–50 g/m²) | Medium‑high | Medium | Curtain coating, paper/plastic lamination |
In IML production, solventless lamination is gradually replacing solvent‑based dry lamination, especially in high‑end food and pharmaceutical packaging. Compared to extrusion lamination, solventless lamination provides a thinner, more uniform adhesive layer and is better suited for bonding PET, aluminium foil, etc. to PE, while extrusion lamination excels at thick coating (e.g., curtain coating).
6. Future Development Trends
Driven by environmental regulations: Global VOC emission limits are becoming increasingly stringent (e.g., China’s Air Pollution Prevention and Control Law, EU Solvent Emissions Directive). Solventless lamination will become the mainstream direction for IML lamination processes.
Development of fast‑curing adhesives: Research into solventless adhesives that achieve “instant curing” or “short curing (<6 hours)” will improve production responsiveness.
Low‑temperature curing types: Designed for heat‑sensitive substrates (e.g., unstretched PE, low‑melting films) to reduce lamination temperature.
Bio‑based solventless adhesives: Use renewable raw materials (e.g., soybean oil, castor oil) to produce polyurethane, reducing dependence on fossil resources.
Digital closed‑loop control: In‑line viscosity monitoring, automatic ratio adjustment, and AI‑based process optimisation will further improve lamination quality stability.
7. Conclusion
The solventless lamination process, with its outstanding advantages of zero VOC emissions, low energy consumption, high speed, and no solvent residue, has become an important direction for environmentally friendly upgrading in IML production. It solves the environmental and safety pain points of traditional solvent‑based dry lamination while meeting the strict requirements for solvent residues in high‑end food and pharmaceutical packaging. Although initial equipment investment and adhesive cost are slightly higher, the overall operating cost (considering energy, environmental facilities, solvent recovery, and production efficiency) is often more competitive.
For IML label converters, transitioning to solventless lamination is not only a passive response to environmental regulations but also a forward‑looking strategy to enhance product competitiveness and expand into high‑end markets. With advances in materials science and automation technology, solventless lamination will occupy an increasingly important position in the future IML industry.
Contact Us
Name*
Telephone*
Region*
Please fill in your request*


